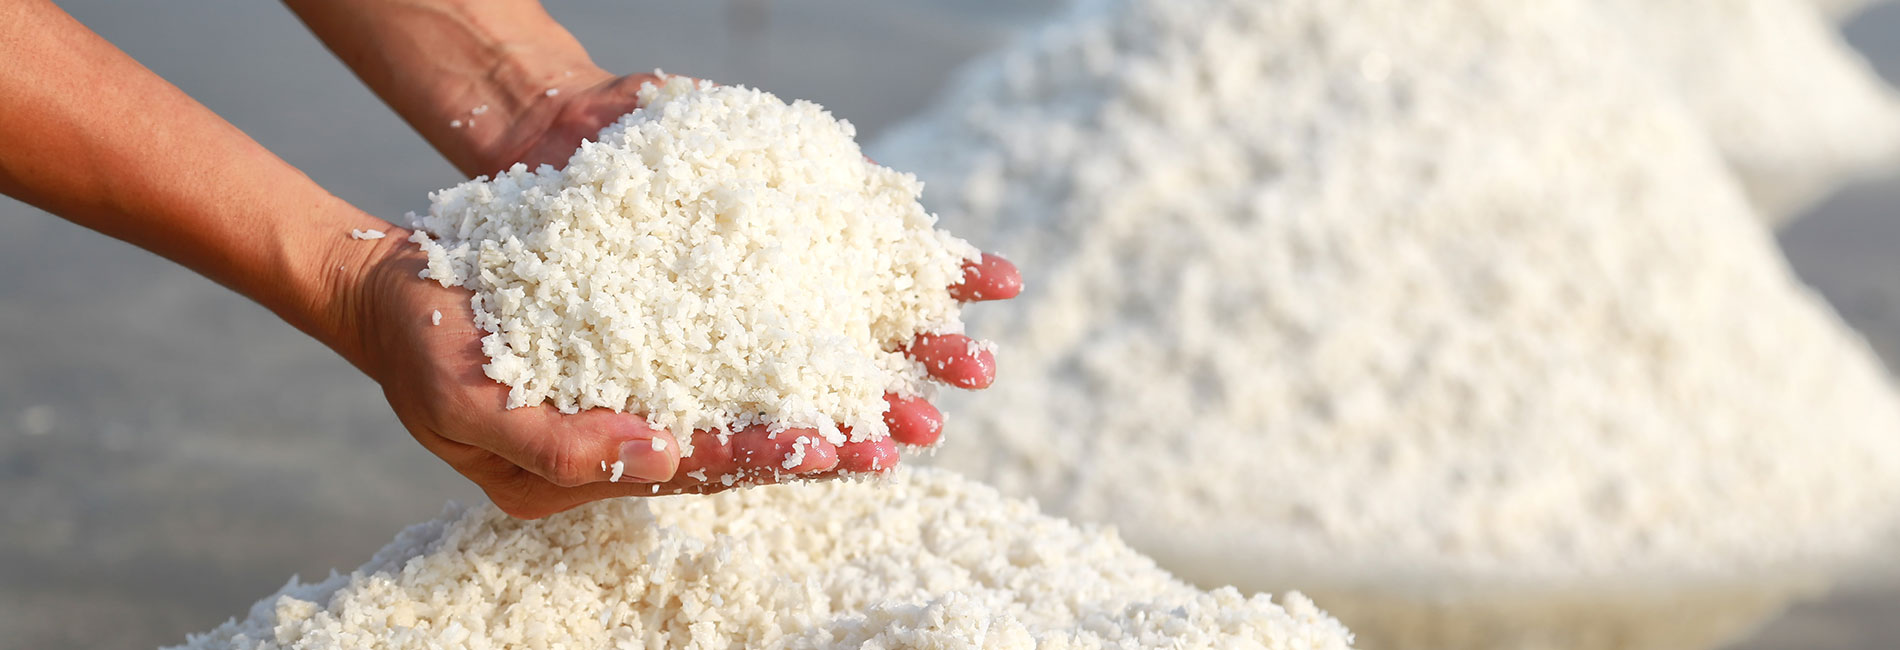
Building pumps for specific or extreme conditions requires years of familiarity with that application. This was especially true for a brine axial flow pump we built for an Australian sea salt production site.
(more…)Side Channel Blowers
Side channel air blowers are a quieter, lower-maintenance alternative to positive displacement lobe blowers. They provide oil-less and contactless compression of gases. The latest generation of blowers offers continuous discharge pressures of up to 1 bar [14.5 psi] and flows of as high as 2,500 cubic metres per hour. Our low-noise blower solutions can help you reduce the cost of acoustic enclosures.
General Features
- Wide range of models to ensure the most efficient selection (e.g., single or double stage; single to triple impellers).
- Different electric motors available, configured in direct, belt, or VSD drive.
- Lower generated noise levels
- Oil-free and contactless manipulation of airflow
- Durable and reliable; little maintenance required
Side Channel Blower Applications
Typical side channel blower applications include:
- Water supply treatment, aeration, and wastewater processing
- Swimming pool filter backwash
- Aquaculture – Fish and shellfish farming
- Large-scale construction and carpentry
- Automatic car wash
- Dental suction systems
- Methane gas extraction
- Soil and groundwater remediation
- Gas emissions monitoring
- Chemical processing
- Dehydration or conditioning of farming produce
- Particle conveyance in food processing – powders, grains, granules, and suspensions
- Carpet cleaning trucks
- Sludge tankers
Available Side Channel Blower Models
Explore our range of side channel blower models designed for industrial performance in Australia. From versatile IEC-compliant motor-powered side channel air blowers to ATEX-rated versions for hazardous environments, our selection delivers efficient, oil-free airflow across a wide spectrum of side channel blower applications.
Electric Motor-Driven Blowers
Our blowers are powered by IEC (International Electrotechnical Commission)-compliant electric motors. Choose from lower cost IE1 standard efficiency, or higher efficiency IE2 and IE3 motors in various blower configurations (i.e., 1, 2, or 3 stage versions).
- Available in single-stage, double-stage, and three-stage versions
- Blower design and electric motor for low noise levels
- IEC-compliant electric motors (IE2, IE3) help minimise overall energy consumption
- Clean oil-free operation and minimal maintenance
ATEX Motor-Powered Blowers
For hazardous requirements, we have side channel blowers with upgraded motors. These blowers have ATEX-compliant motors (compliant with the European Atmosphere Explosible Directive),
- Heavy-duty series
- Available in single-stage, double-stage, and one to three impeller versions
- ATEX-compliant motors for hazardous working environments
- Lower running temperatures
Available variations and configurations
Whichever side channel blower models you choose, we can further systemize the package to suit your particular operation.
- Single stage, [1 impeller]. Ideal for achieving flow rates up to 1000 m³/h, at low pressure/ vacuum levels reaching +/-400 mbar.
- Double stage, [2 impellers in series]. Best used in situations that need limited flow demand, with pressure/ vacuum levels reaching +/-600 mbar.
- Double stage, [2 impellers in parallel]. Double impellers allow for large quantities of suction air up to 1900+ m³/h, with pressure/ vacuum levels reaching +/-400 mbar.
- Three-stage, [3 impellers in series].with pressure/ vacuum levels reaching +/1000 mbar.
- Enhanced safety features. Our blowers are IEC and ATEX compliant. However, if you’re seeking equipment for more demanding or extreme environments, our engineers can further customise your side channel blowers to your specifications. For instance:
- Internal combustion or PTO motor drive.
- Dust ignition-proofing (extra protection or insulation from particle ingress)
- Flameproofing (e.g., built-in flame paths, special inner bearing covers, motor housing to contain internal explosions)
- Non-sparking motors (no sparks or hot surfaces during operation)
- Waterproofing (for applications involving water management, e.g., aquaculture and wastewater remediation)
Case Studies
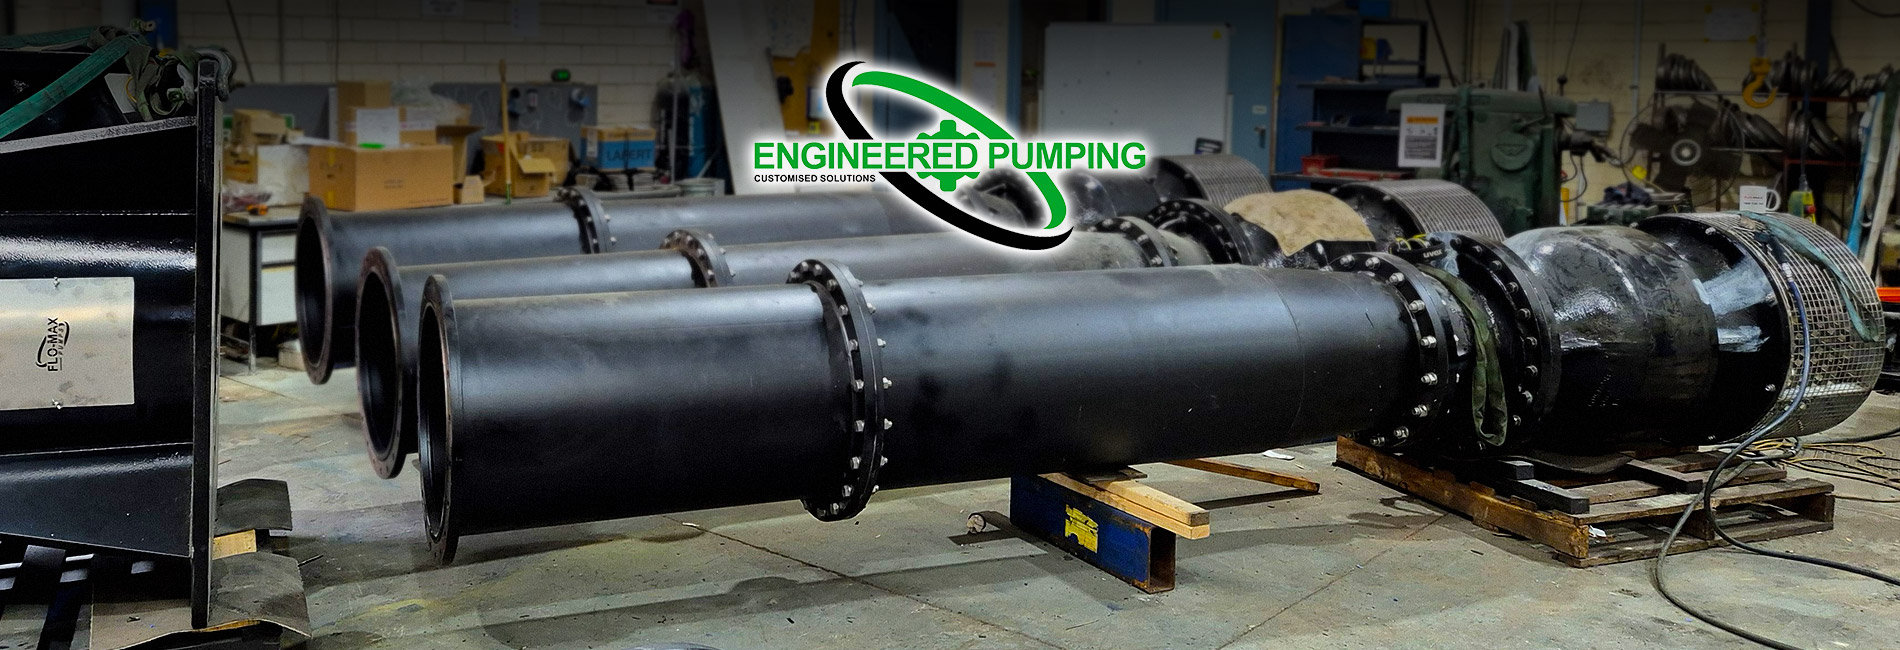
Custom Engineered Industrial Cooling Water Pumps
Recently, we received a request from a nickel processing plant in Central Asia to create large-capacity industrial cooling water pumps. We fulfilled this challenging job order by sourcing rare components and modifying them at our facility.
(more…)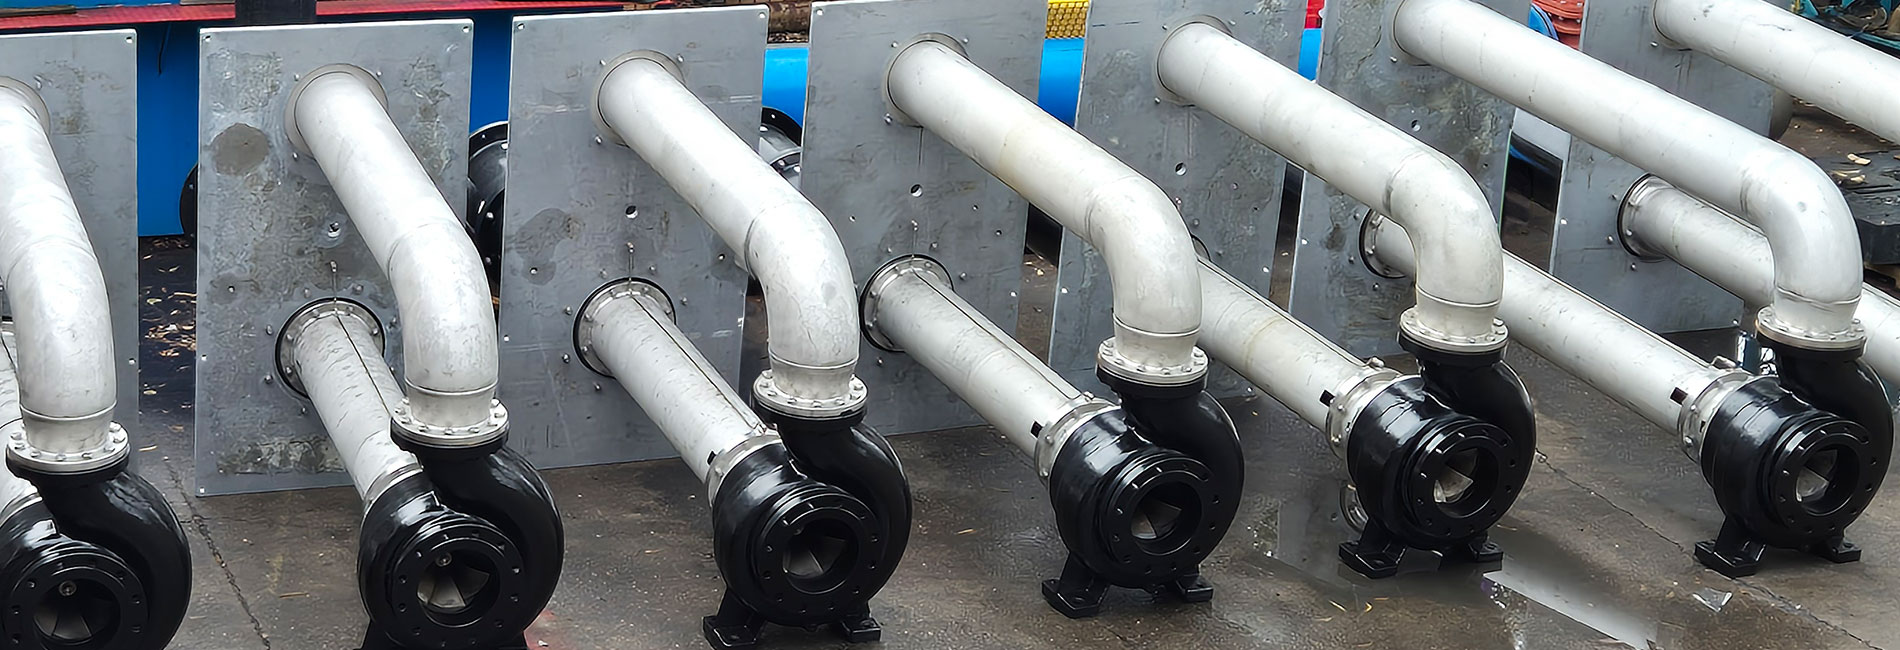
Custom-Built Sump Pumps For A Fuel Import Terminal
A fuel import terminal in NSW needed our help in handling wastewater and seasonal floods at their site. So we custom-built their vertical column sump pumps at our Flo-Max facility.
(more…)Related Products
Explore related solutions tailored to your operational needs.