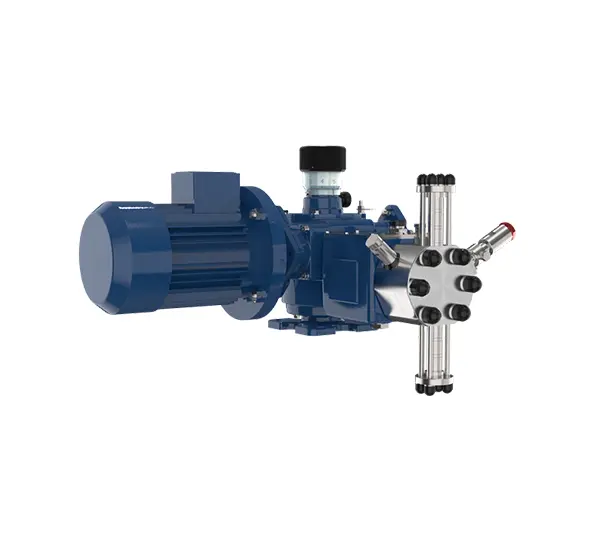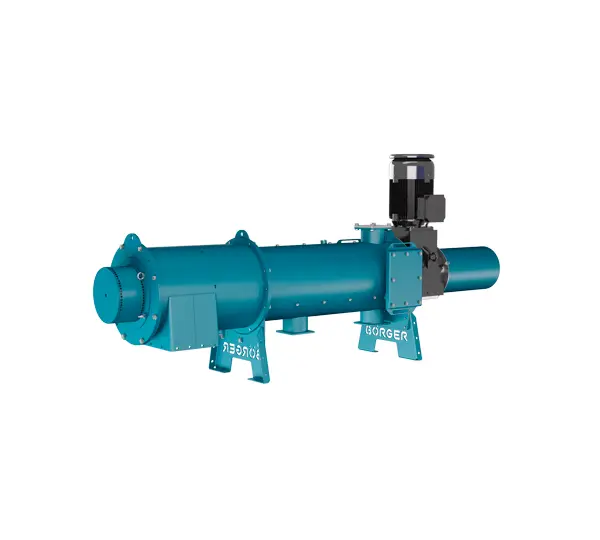
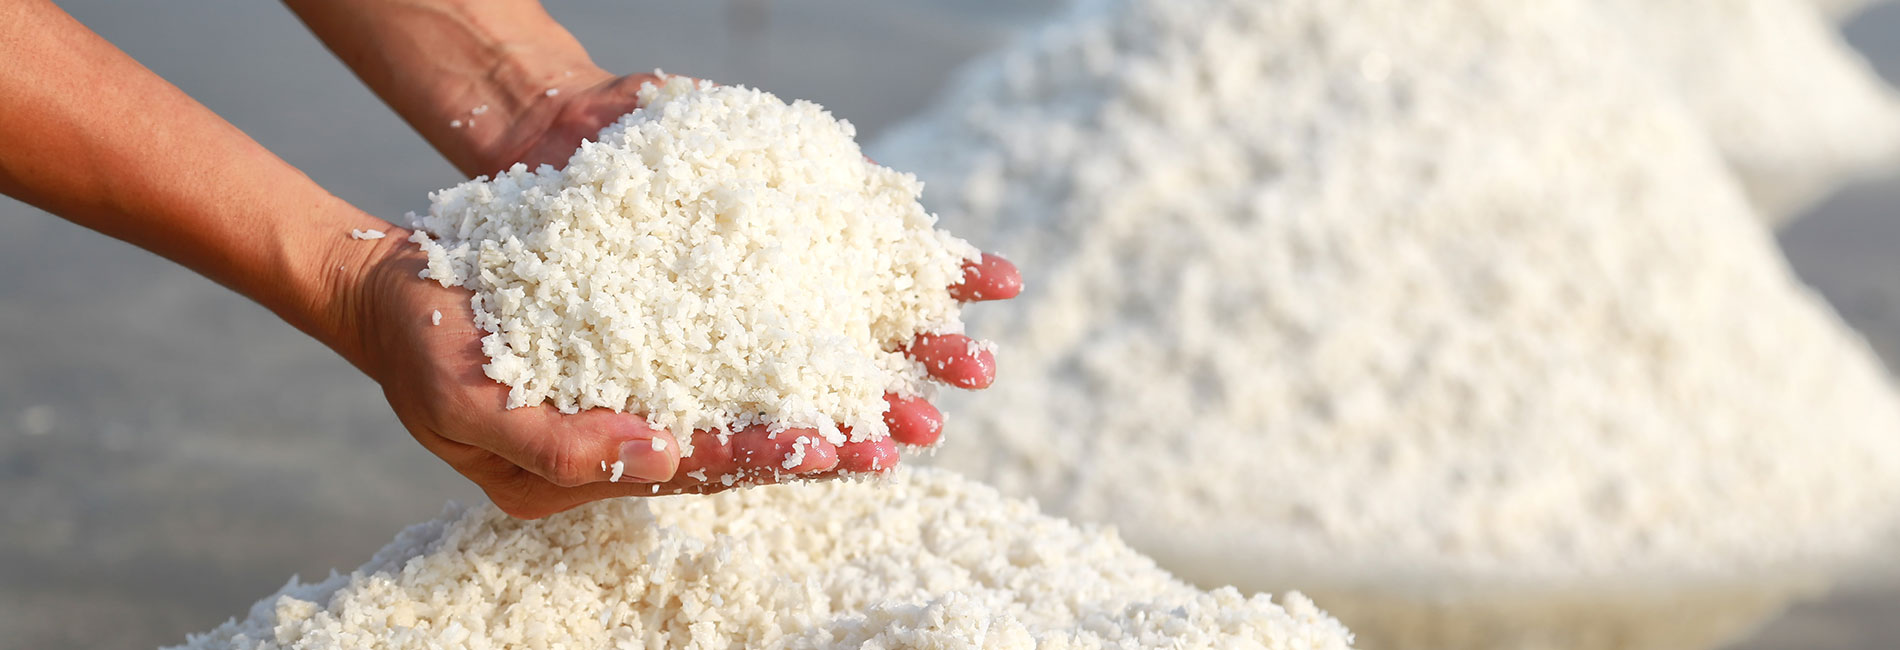
Building pumps for specific or extreme conditions requires years of familiarity with that application. This was especially true for a brine axial flow pump we built for an Australian sea salt production site.
(more…)Rotary Lobe Pumps
Rotary lobe pumps provide reliable, sustained transfer of challenging fluids. These versatile pumps can handle everything from low-viscosity liquids to thick, solids-laden and abrasive media, making them well suited to wastewater, chemical processing, food production, mining and other industries.
We offer rotary lobe pumps in a range of capacities, materials and configurations, including stationary and mobile solutions. Our pump engineering expertise can help you select and configure the right system for your required flow, pressure, fluid characteristics and operating conditions.
Case Studies
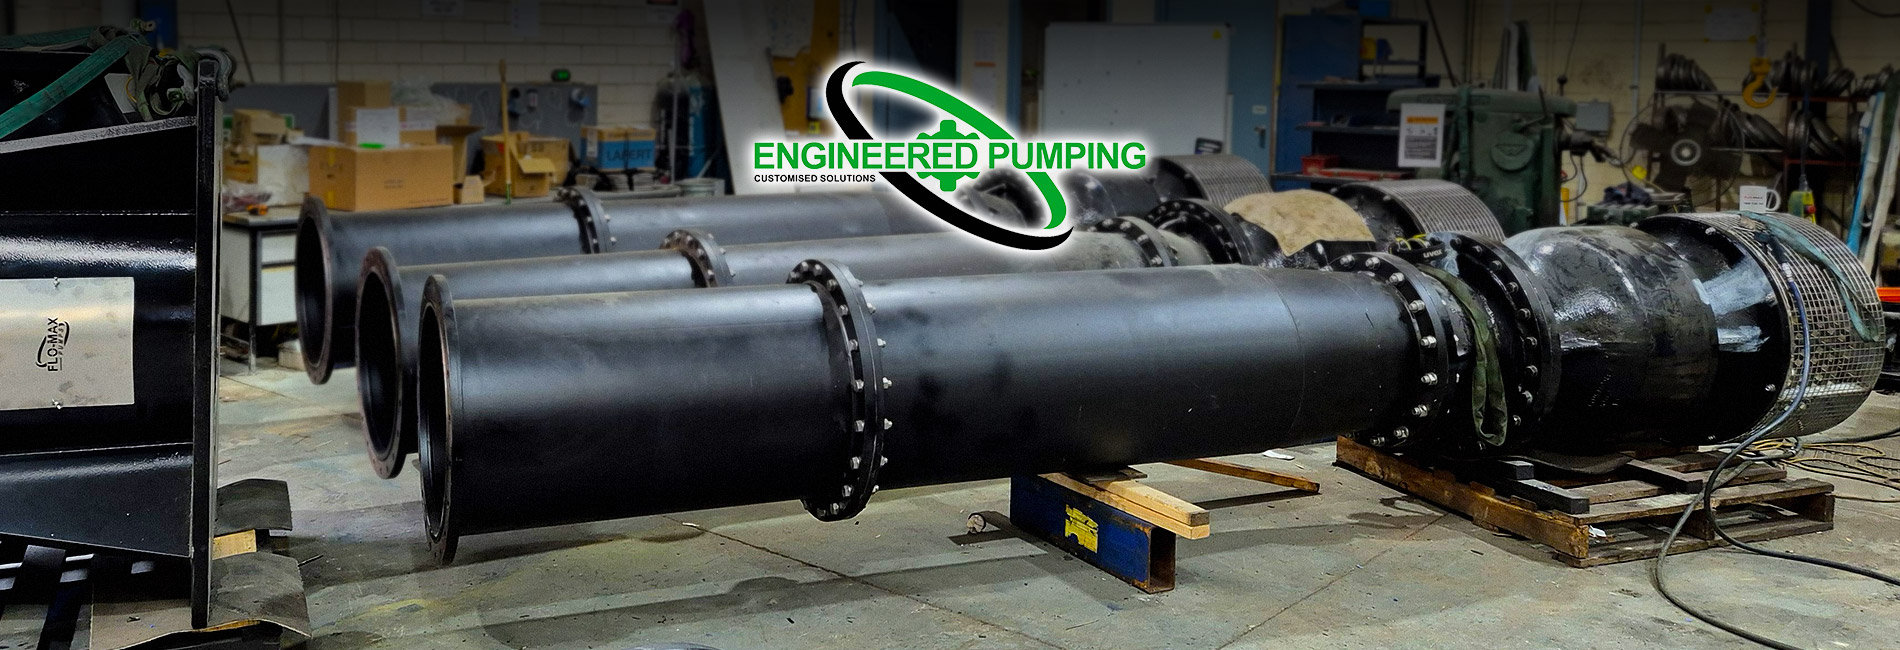
Custom Engineered Industrial Cooling Water Pumps
Recently, we received a request from a nickel processing plant in Central Asia to create large-capacity industrial cooling water pumps. We fulfilled this challenging job order by sourcing rare components and modifying them at our facility.
(more…)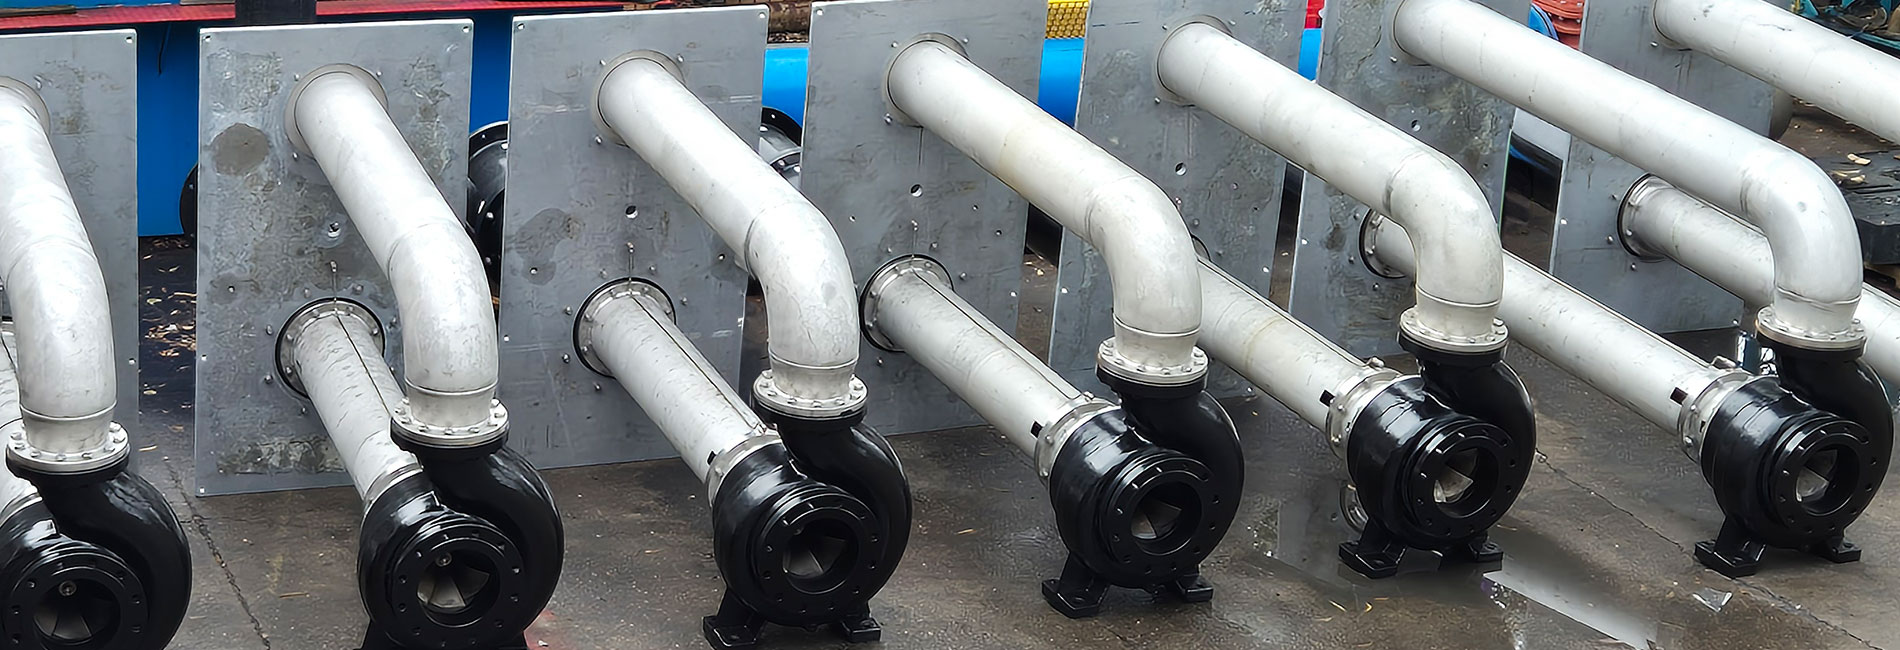
Custom-Built Sump Pumps For A Fuel Import Terminal
A fuel import terminal in NSW needed our help in handling wastewater and seasonal floods at their site. So we custom-built their vertical column sump pumps at our Flo-Max facility.
(more…)Related Products
Explore related solutions tailored to your operational needs.