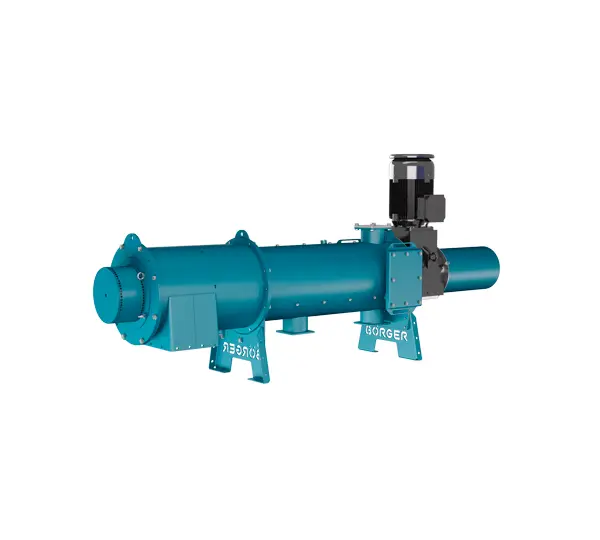
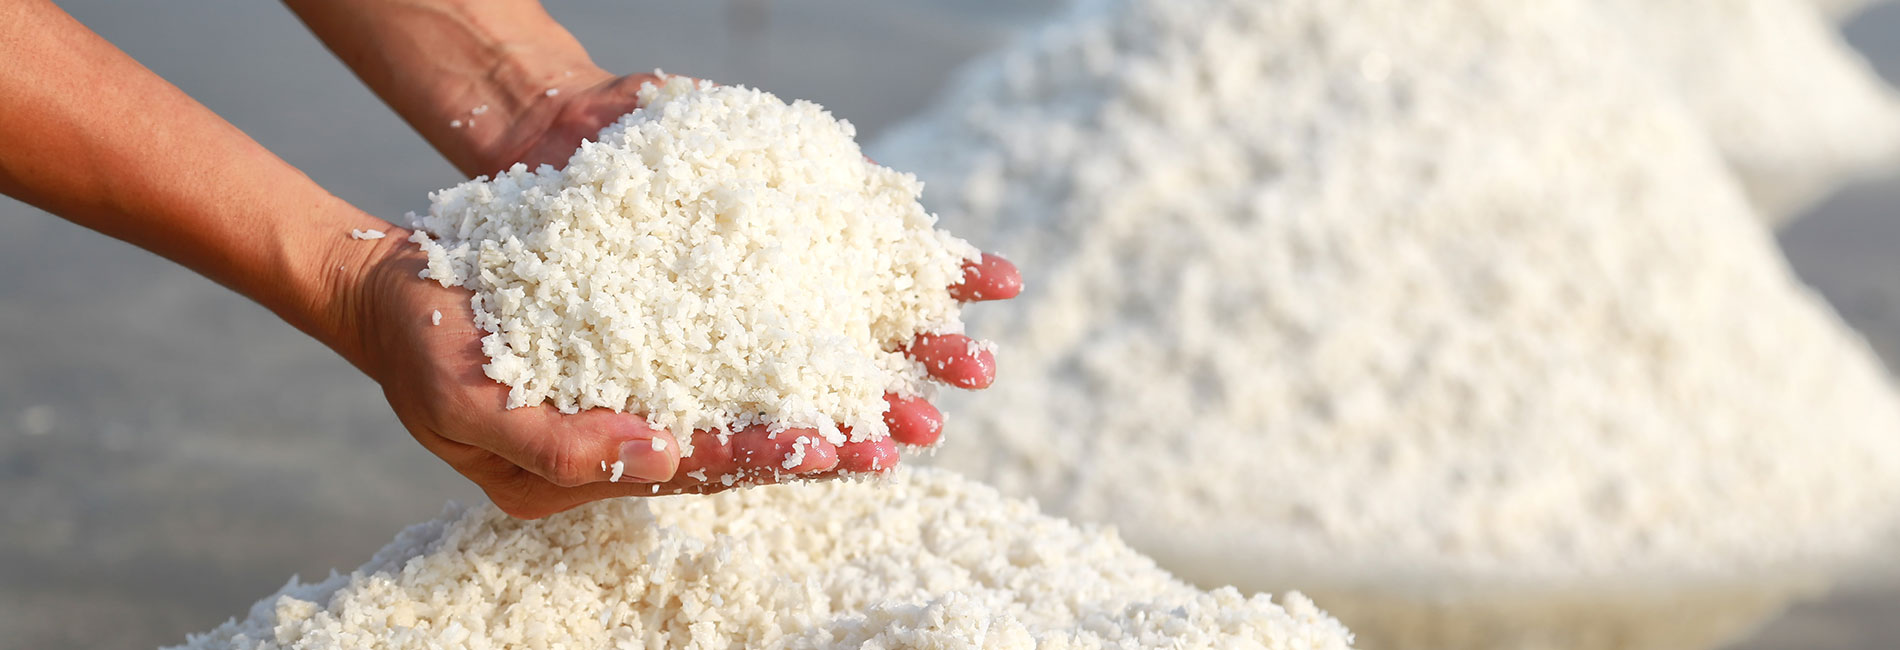
Building pumps for specific or extreme conditions requires years of familiarity with that application. This was especially true for a brine axial flow pump we built for an Australian sea salt production site.
(more…)Blood Bank Refrigerators
Keep your whole blood and blood product inventory at a constant 4°C, with multiple sensors for precise monitoring and temperature programming. The mono-assembly foamed polyurethane insulation and forced air refrigeration system enhance cooling efficiency. Adjustable shelves provide flexible storage for optimal space utilization.
Available Models:
- Movable or stationary
- Single or double doors
- Gross weight sizes: Single doors 103kg, 120kg, 160kg, 175kg, 199kg; Double doors 250kg, 286kg
Case Studies
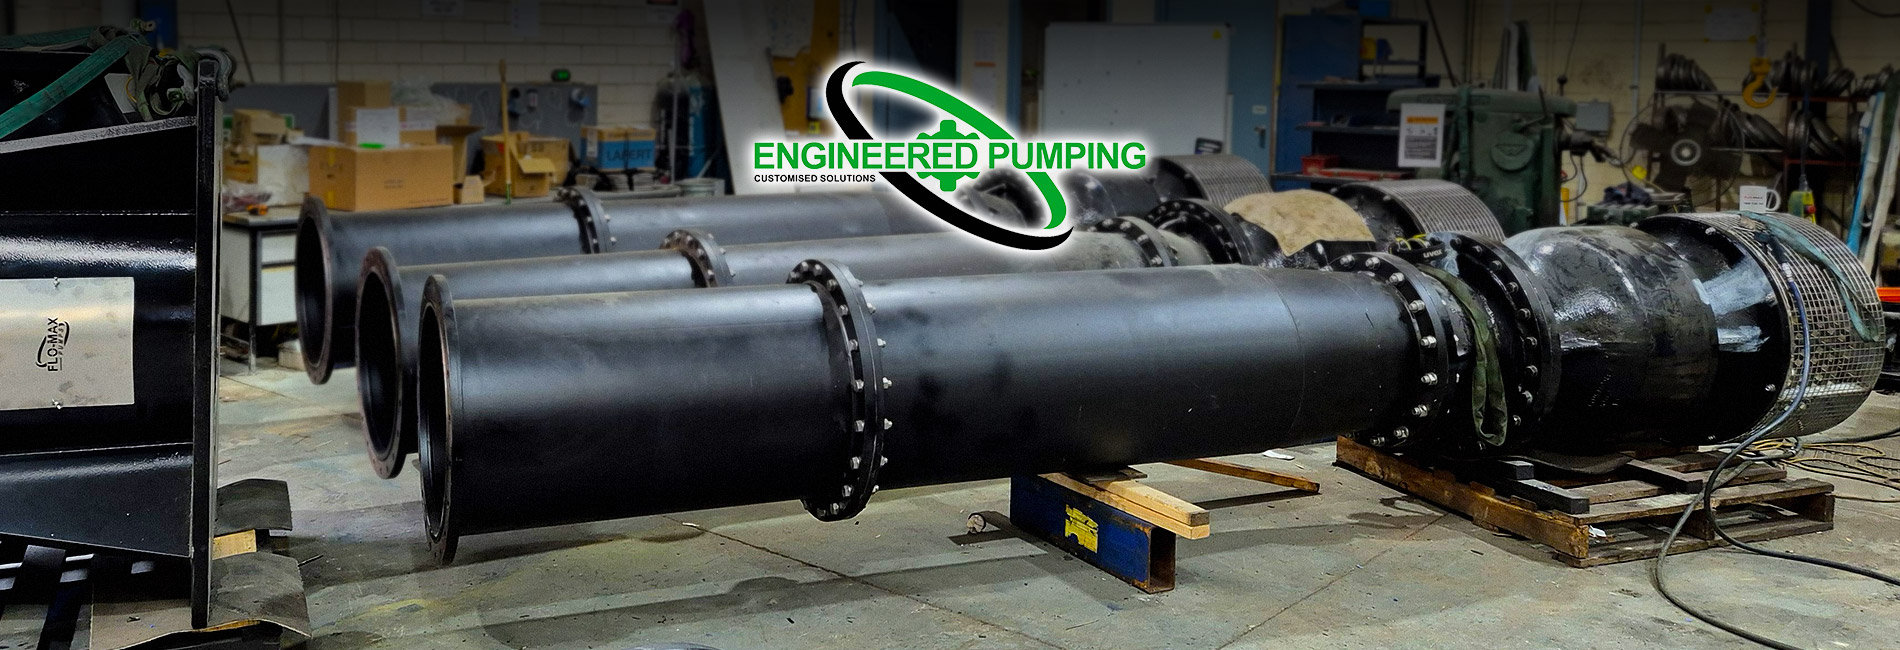
Custom Engineered Industrial Cooling Water Pumps
Recently, we received a request from a nickel processing plant in Central Asia to create large-capacity industrial cooling water pumps. We fulfilled this challenging job order by sourcing rare components and modifying them at our facility.
(more…)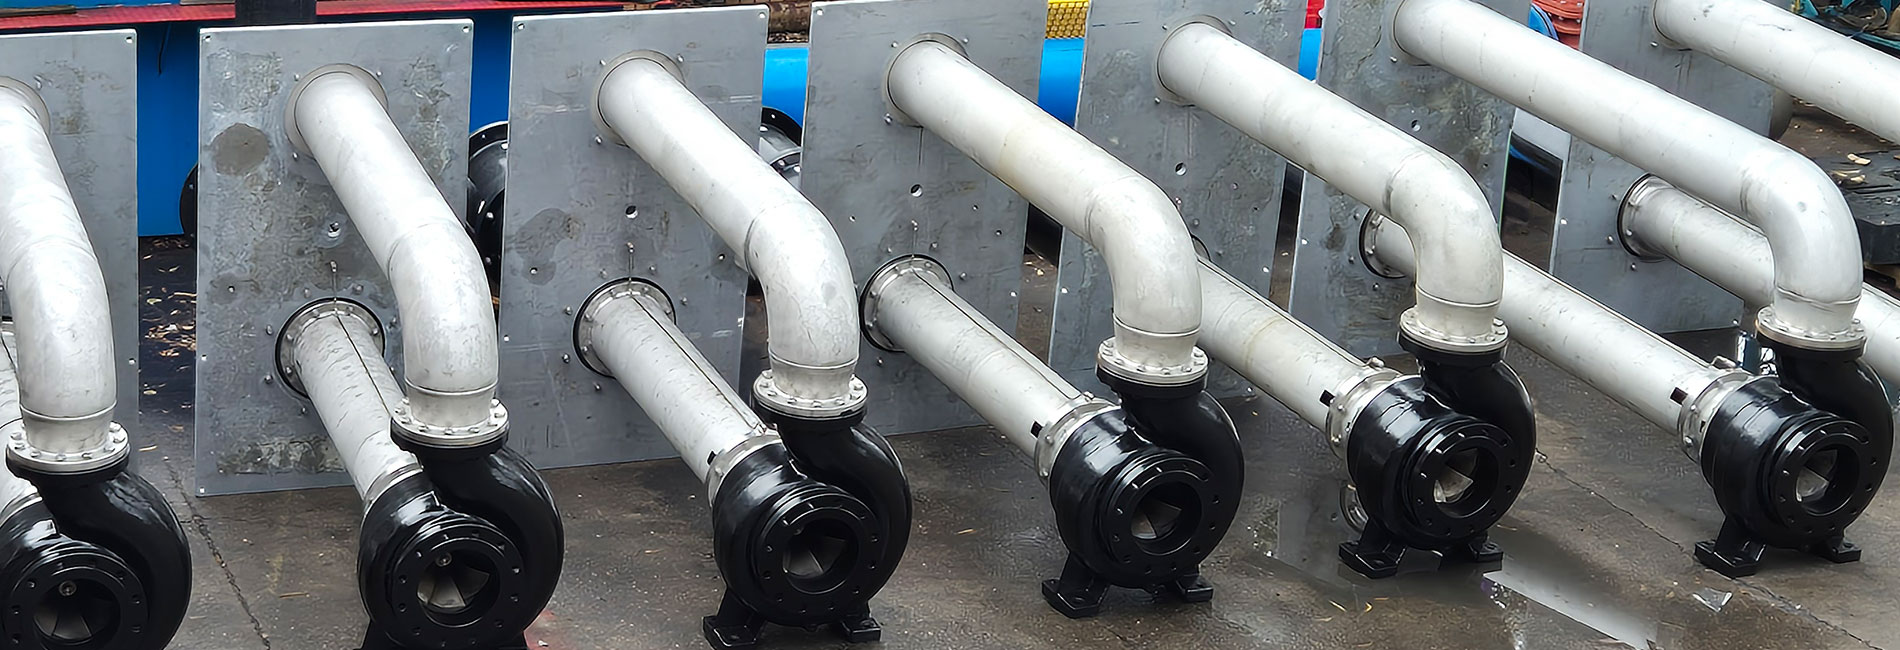
Custom-Built Sump Pumps For A Fuel Import Terminal
A fuel import terminal in NSW needed our help in handling wastewater and seasonal floods at their site. So we custom-built their vertical column sump pumps at our Flo-Max facility.
(more…)Related Products
Explore related solutions tailored to your operational needs.